

What is SSAW Steel Pipe
SSAW (Spiral Submerged Arc Welded Pipe) is a welded steel pipe manufactured by a spiral forming process. The core process is to roll the hot-rolled steel strip into a tube blank at a certain spiral angle (forming angle), and then use submerged arc welding technology to weld the internal and external welds.

SSAW Steel Pipe for Sale
- Common specifications and standards
- Commonly used steel grades: API 5L X42~X100 (yield strength 290~550MPa).
- Steel standards: API 5L, ISO 3183, GB/T 9711.
- Anti-corrosion options: 3PE, coal tar epoxy, galvanized.
SSAW Pipe Manufacture Process Characteristics:
Spiral forming: The steel strip is continuously spirally curled, with high material utilization, suitable for producing large-diameter steel pipes (maximum diameter can reach more than 3 meters).
Submerged arc welding: The welding process is carried out under the flux layer, the weld quality is stable, and it is suitable for the production of thick-walled pipes (wall thickness is usually 6~25.4mm).
Low cost: Compared with straight seam welded pipe (LSAW), spiral welded pipe equipment investment is low and it is suitable for mass production of medium and low-pressure pipelines.
Advanced SSAW Steel Pipe Production Technology

SSAW steel pipe from AGICO are produced with the following technologies.


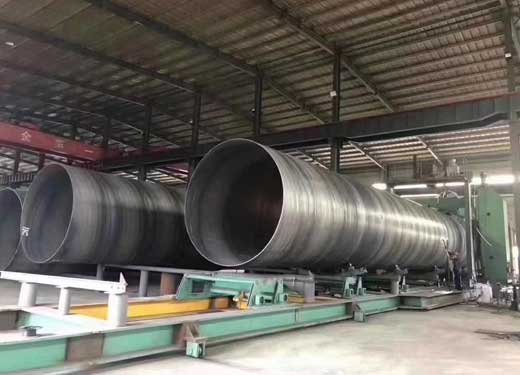
- Production process advantages
- Steel plate pretreatment: sandblasting and rust removal SA2.5 level
- Forming technology: JCOE (straight seam pipe) / spiral rolling (spiral pipe)
- Welding control: multi-wire submerged arc welding (more than 4 wires), weld UT/RT inspection pass rate ≥ 99.5%
- Post-processing: expansion rate 1.5-2.0%, elimination of residual stress
- Performance parameter comparison table
| Property | AGICO SSAW Pipe | Industry Average |
Yield strength deviation | ≤±30MPa | ≤±50MPa |
Low-temperature impact toughness (-30 ℃ ) | ≥100J | ≥60J |
Ovality tolerance | ≤0.5% D | ≤1.0% D |
Main Applications of SSAW Steel Pipe
SSAW steel pipes are widely used in oil, natural gas, water conservancy, construction, chemical industry, electric power, marine and municipal engineering and other fields due to their high strength, corrosion resistance and long life.
Application scenarios:
Onshore medium and low pressure oil and gas long-distance pipelines (pressure is usually ≤12MPa).
Natural gas urban pipeline branch line.
Advantages:
Large diameter (Φ219~Φ3048mm) meets the needs of long-distance transportation.
3PE/FBE anti-corrosion coating can cope with soil corrosion environment.
Oil and Gas Transportation
Application scenarios:
Building foundation pit support piles and bridge pile foundations.
Port terminal support structure.
Advantages:
The spiral weld structure enhances the ability to resist radial pressure.
High diameter-to-thickness ratio (D/t) design saves material.
Structural Support and Pile Foundation
Application scenarios:
Large water pipelines (such as the South-to-North Water Diversion Project).
Municipal water supply/drainage network.
Advantages:
Low cost, suitable for large-span water conservancy projects.
The inner wall is smooth and the water flow resistance is small.
Water Conservancy Projects
Application scenarios:
Large water pipelines (such as the South-to-North Water Diversion Project).
Municipal water supply/drainage network.
Advantages:
Low cost, suitable for large-span water conservancy projects.
The inner wall is smooth and the water flow resistance is small.
Industrial Fluid Transportation
Comparison between SSAW, LSAW and ERW Welded Pipes
If you don’t know which welded pipe to choose, check the comparison info below, and choose by the parameters of diameter, strength and cost:
| Type | SSAW(Spiral Submerged Arc Welded Pipe) | LSAW (Longitudinal Submerged Arc Welded Pipe) | ERW (High Frequency Electric Resistance Welded Pipe) |
Diameter | Φ219~Φ3048mm | Φ219~Φ1420mm | Φ21~Φ660mm |
Strength | Weld strength ≈ 85% of base material | Weld strength ≈ 90% of parent material | Weld strength ≈ 80% of base material |
Cost | Low (high material utilization) | High (wide steel plate required) | middle |
Applicable pressure | Medium and low pressure (≤12MPa) | High pressure (≤20MPa) | Low pressure (≤8MPa) |
Choose SSAW Pipe by Standard
API Standard SSAW Pipe
| The raw material of the SSAW steel pipe includes steel coil, welding wire, flux. All of raw materials must be through strict physical and chemical maintenance before the investment. | ||||||||
| Standard | Grade | Chemical Composition(max)% | Mechanical Properties(min) | |||||
| C | Si | Mn | P | S | Tensile Strength(Mpa) | Yield Strength(Mpa) | ||
| API 5CT | h40 | – | – | – | – | 0.03 | 417 | 417 |
| J55 | – | – | – | – | 0.03 | 517 | 517 | |
| K55 | – | – | – | – | 0.3 | 655 | 655 | |
| API 5L PSL1 | A | 0.22 | – | 0.9 | 0.03 | 0.03 | 335 | 335 |
| B | 0.26 | – | 1.2 | 0.03 | 0.03 | 415 | 415 | |
| X42 | 0.26 | – | 1.3 | 0.03 | 0.03 | 415 | 415 | |
| X46 | 0.26 | – | 1.4 | 0.03 | 0.03 | 435 | 435 | |
| X52 | 0.26 | – | 1.4 | 0.03 | 0.03 | 460 | 460 | |
| X56 | 0.26 | – | 1.4 | 0.03 | 0.03 | 490 | 490 | |
| X60 | 0.26 | – | 1.4 | 0.03 | 0.03 | 520 | 520 | |
| X65 | 0.26 | – | 1.45 | 0.03 | 0.03 | 535 | 535 | |
| X70 | 0.26 | – | 1.65 | 0.03 | 0.03 | 570 | 570 | |
| API 5L PSL2 | B | 0.22 | 0.45 | 1.2 | 0.025 | 0.015 | 415 | 415 |
| X42 | 0.22 | 0.45 | 1.3 | 0.025 | 0.015 | 415 | 415 | |
| X46 | 0.22 | 0.45 | 1.4 | 0.025 | 0.015 | 435 | 435 | |
| X52 | 0.22 | 0.45 | 1.4 | 0.025 | 0.015 | 460 | 460 | |
| X56 | 0.22 | 0.45 | 1.4 | 0.025 | 0.015 | 490 | 490 | |
| X60 | 0.12 | 0.45 | 1.6 | 0.025 | 0.015 | 520 | 520 | |
| X65 | 0.12 | 0.45 | 1.6 | 0.025 | 0.015 | 535 | 535 | |
| X70 | 0.12 | 0.45 | 1.7 | 0.025 | 0.015 | 570 | 570 | |
| X80 | 0.12 | 0.45 | 1.85 | 0.025 | 0.015 | 625 | 625 | |
SSAW Pipe ASTM Standard
| The raw material of the SSAW steel pipe includes steel coil, welding wire, flux. All of raw materials must be through strict physical and chemical maintenance before the investment. | ||||||||
| Standard | Grade | Chemical Composition(max)% | Mechanical Properties(min) | |||||
| C | Si | Mn | P | S | Tensile Strength(Mpa) | Yield Strength(Mpa) | ||
| ASTM A53 | A | 0.25 | 0.1 | 0.95 | 0.05 | 0.045 | 330 | 330 |
| B | 0.3 | 0.1 | 1.2 | 0.05 | 0.045 | 415 | 415 | |
| ASTM A252 | 1 | – | – | – | 0.05 | – | 345 | 345 |
| 2 | – | – | – | 0.05 | – | 414 | 414 | |
| 3 | – | – | – | 0.05 | – | 455 | 455 | |
SSAW Pipe EN Standards:
| The raw material of the SSAW steel pipe includes steel coil, welding wire, flux. All of raw materials must be through strict physical and chemical maintenance before the investment. | ||||||||
| Standard | Grade | Chemical Composition(max)% | Mechanical Properties(min) | |||||
| EN10217-1 | P195TR1 | 0.13 | 0.35 | 0.7 | 0.025 | 0.02 | 320 | 320 |
| P195TR2 | 0.13 | 0.35 | 0.7 | 0.025 | 0.02 | 320 | 320 | |
| P235TR1 | 0.16 | 0.35 | 1.2 | 0.025 | 0.02 | >360 | >360 | |
| P235TR2 | 0.16 | 0.35 | 1.2 | 0.025 | 0.02 | >360 | >360 | |
| P265TR1 | 0.2 | 0.4 | 1.4 | 0.025 | 0.02 | 410 | 410 | |
| P265TR2 | 0.2 | 0.4 | 1.4 | 0.025 | 0.02 | 410 | 410 | |
| EN10217-2 | P195GH | 0.13 | 0.35 | 0.7 | 0.025 | 0.02 | 320 | 320 |
| P235GH | 0.16 | 0.35 | 1.2 | 0.025 | 0.02 | >360 | >360 | |
| P265GH | 0.2 | 0.4 | 1.4 | 0.025 | 0.02 | 410 | 410 | |
| EN10217-5 | P235GH | 0.16 | 0.35 | 1.2 | 0.025 | 0.02 | >360 | >360 |
| P265GH | 0.2 | 0.4 | 1.4 | 0.025 | 0.02 | 410 | 410 | |
| EN10219-1 | S235JRH | 0.17 | – | 1.4 | 0.04 | 0.04 | >360 | >360 |
| S275JOH | 0.2 | – | 1.5 | 0.035 | 0.035 | 410 | 410 | |
| S275J2H | 0.2 | – | 1.5 | 0.03 | 0.03 | 410 | 410 | |
| S355JOH | 0.22 | 0.55 | 1.6 | 0.035 | 0.035 | 470 | 470 | |
| S355J2H | 0.22 | 0.55 | 1.6 | 0.03 | 0.03 | 470 | 470 | |
| S355K2H | 0.22 | 0.55 | 1.6 | 0.03 | 0.03 | 470 | 470 | |
SSAW Pipe Dimension Chart
| Steel Pipe Outer Diameter | A and Below~A | L245 (B) | L290 (X42) | L320 (X46 ) | L360 (X52) | L390 (X56) | L415 CX60) | L450 (X65) | L485 (X70) | L555 (X80) | L625 (X90) | L690 (XI00) | Length ( m ) | |
| Inch | mm | |||||||||||||
| 8.625 | 219.1 | 5.6 ~10.3 | 5.6~10.3 | 5.6~7.1 | 5.6 ~7.1 | 5.6~7.1 | 8.0~12.5 | |||||||
| 10.75 | 273.1 | 5.6~10.3 | 5.6~10.3 | 5.6~9.5 | 5.6~8.5 | 5.6~8.5 | 8.0~12.5 | |||||||
| 12.79 | 325 | 5.6 ~10.3 | 5.6 ~10.3 | 5.6 ~10.3 | 5.6 ~9.5 | 5.6 ~9.5 | 5.6 ~8.7 | 8.0~13.0 | ||||||
| 14 | 355.6 | 5.6~11.9 | 5.6~1 1.9 | 5.6~10.3 | 5.6~9.5 | 5.6~9.5 | 5.6~8.7 | 8.0~13.0 | ||||||
| 16 | 406.4 | 5.6 ~12.7 | 5.6~12.7 | 5.6~12.7 | 5.6~12.7 | 5.6 ~12.7 | 5.6 ~1 1.9 | 5.6~1 1.9 | 5.6~1 1.9 | 5.6~1 1.9 | 8.0~13.0 | |||
| 18 | 457 | 5.6~12.7 | 5.6~12.7 | 5.6~12.7 | 5.6~12.7 | 5.6~12.7 | 5.6~1 1.9 | 5.6~1 1.9 | 5.6~1 1.9 | 5.6 ~1 1.9 | 8.0~13.0 | |||
| 20 | 508 | 5.6~14.3 | 5.6 ~14.3 | 5.6 ~14.3 | 5.6~14.3 | 5.6~14.3 | 5.6~14.3 | 5.6 ~ 14.3 | 5.6~12.7 | 5.6 ~12.7 | 8.0~13.0 | |||
| 22 | 559 | 5.6 ~14.3 | 5.6~14.3 | 5.6~14.3 | 5.6 ~14.3 | 5.6 ~14.3 | 5.6~14.3 | 5.6~14.3 | 5.6~12.7 | 5.6 ~12.7 | 5.6~11.1 | 8.0~13.0 | ||
| 24 | 610 | 6~17.48 | 6~17.48 | 6~17.48 | 6~ 17.48 | 6~17.48 | 6~ 17.48 | 6~ 17.48 | 6~17.48 | 6 ~17.48 | 6~17.48 | 6~17.48 | 6 ~15.88 | 8.0 ~15.0 |
| 26 | 660 | 6~18.4 | 6~18.4 | 6~18.4 | 6 ~18.4 | 6~18.4 | 6 ~18.4 | 6~18.4 | 6~18.4 | 6~18.4 | 6~17.48 | 6~17.48 | 6~ 17.48 | 8.0~15.0 |
| 28 | 711 | 6~18.4 | 6~18.4 | 6~18.4 | 6~18.4 | 6~18.4 | 6~18.4 | 6~18.4 | 6~18.4 | 6 ~18.4 | 6~ 17.48 | 6~17.48 | 6~ 17.48 | 8.0~15.0 |
| 30 | 762 | 7.1~20.62 | 7.1 ~20.62 | 7.1~20.62 | 7.1~20.62 | 7.1~20.62 | 7.1~20.62 | 7.1~20.62 | 7.1~20.62 | 7.1~20.62 | 7.1 ~ 19.05 | 7.1 ~ 19.05 | 7.1 ~19.05 | 8.0~15.0 |
| 32 | 813 | 7.1~22.23 | 7.1~22.23 | 7.1~22.23 | 7.1~22.23 | 7.1~22.23 | 7.1~22.23 | 7.1~22.23 | 7.1~22.23 | 7.1~22.23 | 7.1~20.62 | 7.1~20.62 | 7.1~20.62 | 8.0~15.0 |
| 36 | 914 | 7.1~25.4 | 7.1~25.4 | 7.1~25.4 | 7.1~25.4 | 7.1 ~25.4 | 7.1~25.4 | 7.1~25.4 | 7.1~25.4 | 7.1~25.4 | 7.1~22.23 | 7.1~22.23 | 7.1 ~22.23 | 8.0~15.0 |
| 40 | 1016 | 7.9~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9 ~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9~22.23 | 7.9~22.23 | 7.9~22.23 | 8.0~15.0 |
| 42 | 1067 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9 ~ 25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~22.23 | 7.9~22.23 | 7.9 ~22.23 | 8.0~15.0 |
| 44 | 1118 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9 ~22.23 | 7.9 ~22.23 | 7.9~22.23 | 8.0~15.0 |
| 46 | 1 168 | 7.9~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~22.23 | 7.9~22.23 | 7.9~22.23 | 8.0 ~15.0 |
| 48 | 1219 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9 ~22.23 | 7.9 ~22.23 | 7.9~22.23 | 8.0~15.0 |
| 52 | 1321 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~22.23 | 7.9~22.23 | 7.9~22.23 | 8.0~15.0 |
| 56 | 1422 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 8.0~15.0 |
| 60 | 1524 | 7.9 ~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~ 25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9 ~ 25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9 ~25.4 | 8.0~15.0 |
| 64 | 1626 | 7.9 ~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9 ~25.4 | 7.9 ~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 7.9~25.4 | 8.0~15.0 |
| 6s | 1727 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9~18 | 7.9~16 | 8.0~13.0 | ||
| 72 | 1829 | 7.9~20 | 7.9~20 | 7.9~20 | 7.9 ~20 | 7.9~20 | 7.9~20 | 7.9~20 | 7.9~20 | 7.9~18 | 7.9 ~16 | 8.0~13.0 | ||
| 76 | 1930 | 7.9 ~20 | 7.9~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 79 ~20 | 7.9 ~20 | 7.9 ~18 | 7.9 ~16 | 8.0~13.0 | ||
| 80 | 2032 | 7.9 ~20 | 7.9~20 | 7.9~20 | 7.9~20 | 7.9~20 | 7.9~20 | 7.9~20 | 7.9~20 | 7.9~18 | 7.9~16 | 8.0~13.0 | ||
| 84 | 2134 | 7.9~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9 ~20 | 7.9~18 | 7.9~16 | 8.0~13.0 | ||
